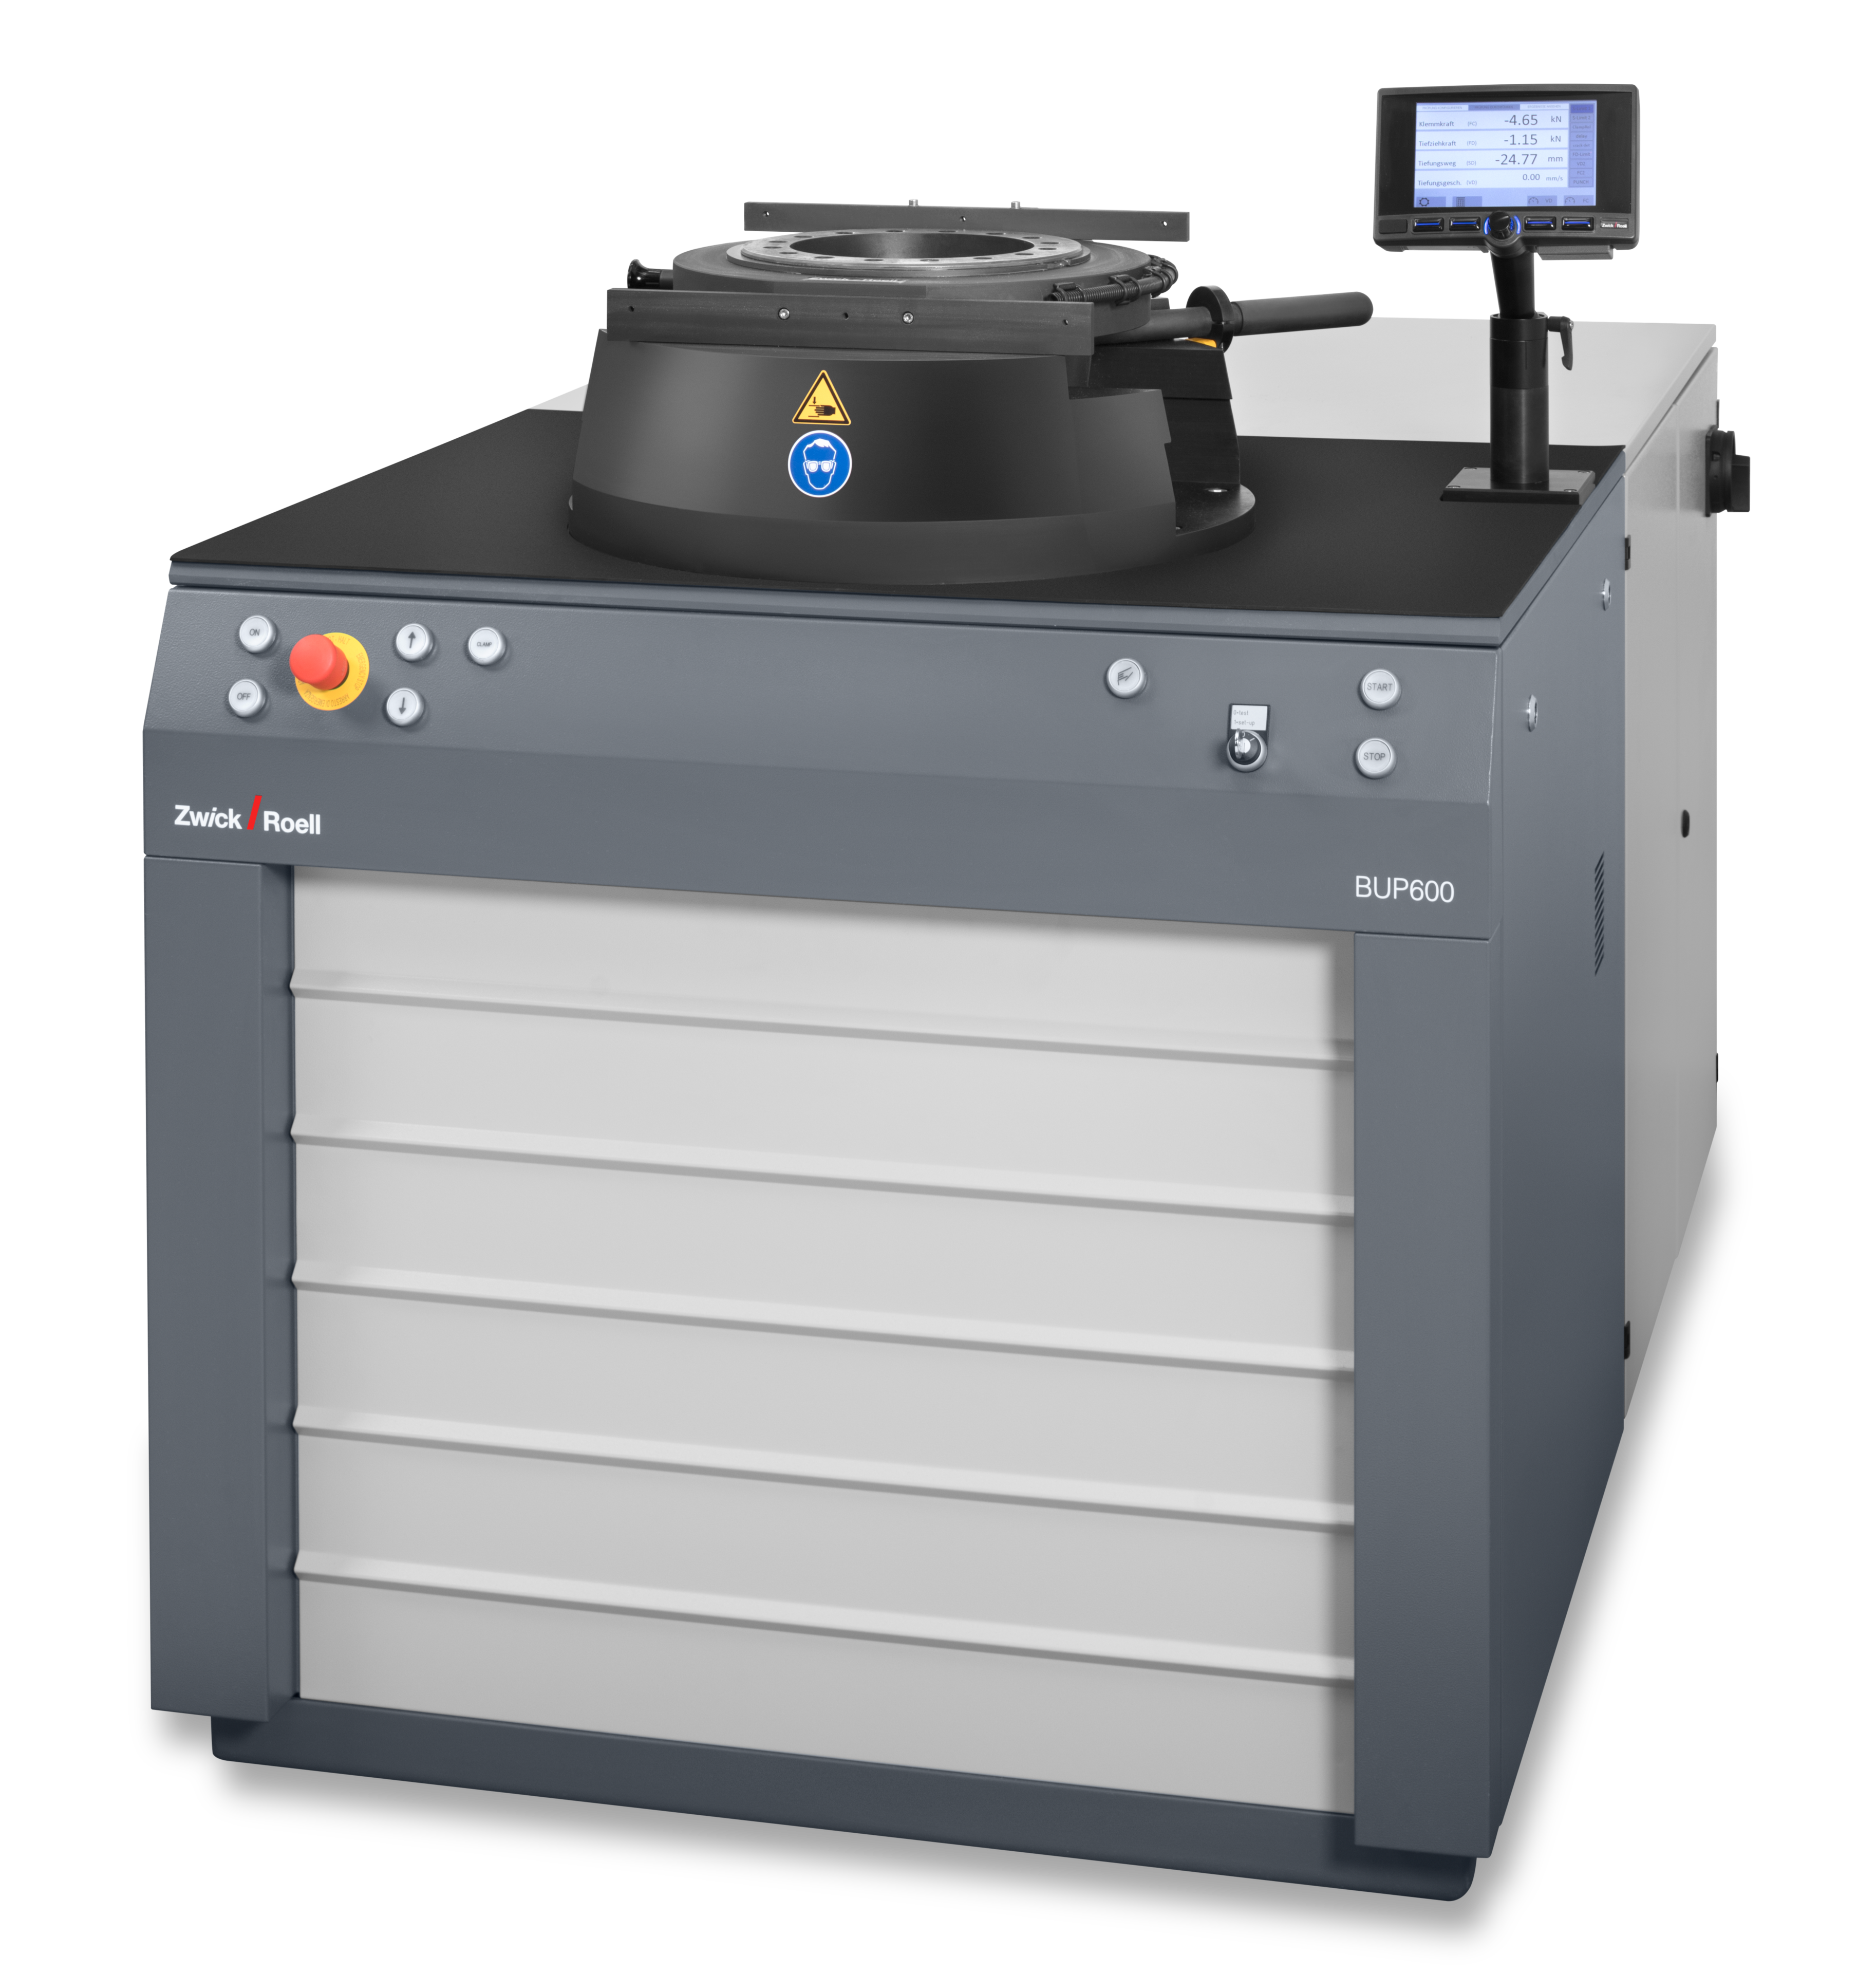
Bulge test to ISO 16808
The hydraulic bulge test to ISO 16808 is a test method used in materials testing for the determination of sheet metal forming properties.
In a bulge test biaxial stress-strain curves are determined on sheet metals using a hydraulic cupping test. A metal blank (specimen) is fully clamped between the die and the blank holder. Under the specimen there is a chamber with oil. The drawing punch pushes the oil up. The continuously increasing oil pressure leads to a curvature in the specimen. The test is run until a crack occurs.
Following the bulge test to ISO 16808, the flow curve can be determined. For this the oil pressure, the evolution of the sheet metal thickness during the test and the optical measurement and assessment of the curvature in the sheet metal are evaluated.
The test is similar to the FLC test with Nakajima die. The cupping procedure however, takes place without friction.

Bulge test with strain rate control
For the bulge test in accordance with DIN EN ISO 16808, a constant strain rate is recommended. With ZwickRoell sheet metal testing machines, the strain rate can be controlled precisely. This function is optionally available through the testXpert testing software.
In practice, this function is used, for example, at Speira's Research and Development Center in Bonn, Germany, to perform bulge tests.
The setpoint is specified via the testXpert software. During the test, the testing system receives measurement data from the external ARAMIS camera system by GOM and adjusts the punch speed accordingly. The measurement results are recorded in GOM as well as testXpert.
For the bulge test with constant strain rate recommended in DIN EN ISO 16808, up to ten preset piston-speed values can be stored in the sheet metal testing machine's PLC. This allows the piston speed to be specifically adjusted during the course of the test. For special testing requirements, the piston speed can also be controlled via an output signal from the DIC system used.